Engineered Cable Tray Accessories for Russian Projects
Pre-galvanized and hot-dip continuous steel protection accessories engineered for automated field erection, rapid bolt alignment, and reinforced structural containment under severe snow and wind loads.
GOST 15150-69 HL1 Compliant
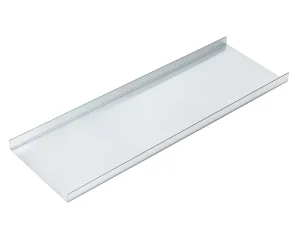
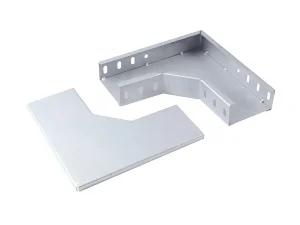
Pre-Galvanized Cable Tray Cover Cable Protection
Flanged, snap-on, and bolt-secured pre-galvanized covers preventing heavy ice accumulation, snow loading, and UV cable degradation across open Russian industrial rack spans.
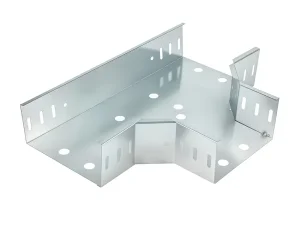
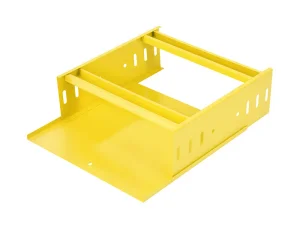
Factory-formed curved transitions (90° horizontal elbows, equal tees, crosses) guaranteeing strict minimum cable bend radius control for MV/HV power cabling.
A comprehensive examination of electrical containment infrastructure across the Russian Federation, highlighting the Eastern Sourcing Corridor, regulatory requirements under GOST R 52868-2007, and massive petrochemical investments.
The Supply Chain Realignment
Following structural shifts in international trade, Russian engineering, procurement, and construction (EPC) conglomerates have decisively transitioned from Western European suppliers to Tier-1 Chinese manufacturing powerhouses. The focus has moved toward long-term manufacturing agreements capable of sustaining massive metallurgy and chemical refining programs without logistical disruption.
Import Substitution: Replacing traditional Western brands with high-precision, automated manufacturing equivalents.
Cross-Border Logistics: Streamlined rail corridors via Manzhouli, Zabaikalsk, and direct sea freight to Vladivostok and St. Petersburg.
Contracting Flexibility: Direct settlement in non-restricted currencies, stabilizing multi-million dollar capital expenditure frameworks.
GOST-R 52868-2007 & Fire Safety
In the Russian market, standard commercial cable management hardware fails to meet rigorous regional statutory codes. Cable tray accessories must comply strictly with GOST R 52868-2007 (Cable Tray Systems and Cable Ladder Systems for Electrical Installations) and GOST 30247.0-94 regarding fire endurance.
Electrical Continuity: Maximum contact impedance across splice plates ≤ 50 mΩ to avoid arcing during fault surges.
Circuit Integrity (E90): Retention of physical cabling containment under standard temperature curve testing up to 90 minutes.
Mechanical Safe Working Load (SWL): Minimum safety factor of 1.7× under distributed static dead load + accumulated dynamic snow loading.
Mega-Projects Driving Consumption
Massive capital deployment across the Arctic Circle, Western Siberia, the Far East, and the Baltic coast drives unprecedented demand for high-durability accessories. High capital velocity in natural gas liquefaction, mineral extraction, and power grid automation dictates massive accessory consumption.
LNG Complexes: Yamal LNG, Arctic LNG 2, and Baltic LNG requiring deep cryogenic-resistant and marine-grade stainless hardware.
Mining & Smelting: Norilsk Nickel, Udokan Copper, and ALROSA facilities requiring SO&sub2; and acid-mist resilient coatings.
Trans-Siberian Modernization: Power rail electrification calling for heavy vibration-proof strut channels and reinforced support arms.
Standard commercial carbon steel undergoes a catastrophic ductile-to-brittle transition when exposed to typical Russian winter temperatures dropping from -30°C to -60°C. Conventional stamping steels shatter under seismic vibration, mechanical wind buffeting, and heavy snow drifts.
Shanghai Qiongkai utilizes high-strength low-alloy structural steels engineered with optimized carbon equivalents and micro-alloyed with Vanadium and Niobium (comparable to Russian standard steel grade 09G2S). Our cold-formed accessories undergo rigorous Charpy V-notch impact testing at -60°C, retaining minimum impact energy absorption exceeding 34 J/cm².
GOST 15150-69 Climatic Execution: UHL1 / HL1Our cable tray accessories are certified for outdoor operations in cold and temperate microclimatic zones with absolute temperature minimums down to -60°C, resisting brittle structural shearing under high ice accretion.
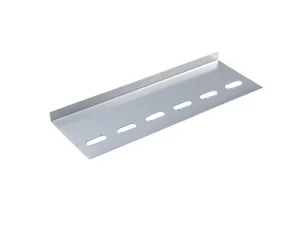
Furthermore, differential thermal expansion is calculated systematically. In a continuous 300-meter petrochemical pipe rack span, seasonal temperature deltas (ΔT = 80°C between summer and winter) cause severe longitudinal contraction. Our variable-slotted expansion guide plates accommodate up to 45 mm of axial movement while maintaining continuous earth bonding.
Corrosion Category (ISO 12944)
Russian Environment (GOST 15150)
Recommended Accessory Material / Finish
Nominal Service Life
C2 (Low)
Enclosed dry facilities, standard warehouses (U3)
Pre-Galvanized Steel (PG) Z275 (20 μm)
25+ Years
C3 (Medium)
Urban industrial, high humidity interiors (U1)
Electro-Galvanized + Powder Coating (RAL)
20+ Years
C4 (High)
Heavy industrial zones, coastal ports (UHL1)
Hot-Dip Galvanized (HDG) ≥65 μm (ISO 1461)
30+ Years
C5-I / C5-M (Extreme)
Chemical refineries, Arctic offshore, nickel smelters
HDG ≥85 μm or Stainless Steel SS316L / 1.4404
40+ Years
CX (Severe Offshore)
Arctic LNG open terminals, marine splash zones
Fiberglass Reinforced Polymer (FRP) / Super Duplex
50+ Years
Industry 4.0 Advanced Manufacturing Ecosystem
China Factory 4.0: Unmatched Supply Chain Resilience & Capacity
Shanghai Qiongkai Industry Co., Ltd. operates a high-precision, automated manufacturing complex designed to meet the strictest technical requirements of global and Russian EPC infrastructure contractors.
Automated High-Speed Stamping & Roll-Forming
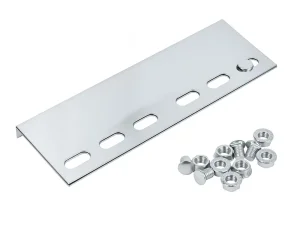
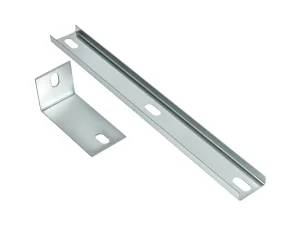
Our Shanghai facility hosts over 60 heavy-duty precision stamping presses and 12 continuous cold roll-forming lines. Automated progressive stamping dies produce cable tray brackets, L-hangers, splice plates, and hold-down clamps with micron-level tolerances (±0.15 mm), ensuring immediate hole alignment in -40°C field environments where re-drilling is impossible.
Eco-Friendly Smart Galvanizing Line
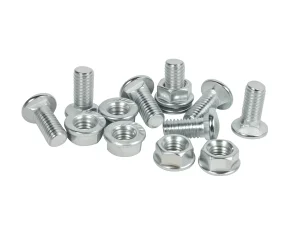
Our centralized hot-dip galvanizing operations adhere strictly to ISO 1461 and ASTM A123 standards. Utilizing automated flux baths and centrifuge spinning processes, we achieve uniform zinc coatings exceeding 85 μm without leaving burrs, sharp icicles, or thread-clogging deposits on bridge frame screws, threaded rods, or locking nuts.
Digital MES & Traceable Quality Control
Every accessory production batch is tracked via an integrated Manufacturing Execution System (MES). From raw steel coil spectrometer analysis (confirming chemical composition, P/S thresholds, and low-alloy chemistry) to salt spray testing (exceeding 1000 hours per ASTM B117), our QA team provides comprehensive Mill Test Certificates (EN 10204 3.1).
Field Deployment Case Matrix
Engineered for Russia’s Most Demanding Operational Arenas
From the permafrost tundra of the Yamal Peninsula to high-vibration metallurgical smelters in the Urals, discover how Qiongkai accessories ensure zero-failure electrical distribution.
Yamal & Gydan LNG Liquefaction Modules
Modular LNG plants constructed on sub-zero permafrost require vibration-dampened strut channel attachments, seismic cable cleats, and heavy-duty 316L stainless steel trunking covers capable of enduring continuous Arctic wind shears and high-salinity maritime exposure.
Western Siberia Oil & Gas Refineries
Corrosive sulfur dioxide (SO&sub2;) and hydrogen sulfide (H&sub2;S) gases in petrochemical downstream facilities attack standard electroplate coatings. Our double-dip hot-dip galvanized (HDG) and powder-coated hybrid finishes prevent premature red rust across multi-tier ladder rack runs.
Ural Metallurgical & Heavy Smelting Mills
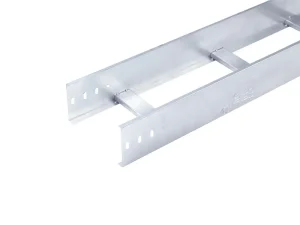
Extreme thermal cycling, mechanical impact risks, and airborne particulate accumulation demand reinforced molded cable tray fittings with integrated solid covers and high-tensile bridge frame locking screws that prevent accidental dislodgement.
Moscow & St. Petersburg Hyperscale Data Centers
Rapid deployment of wire mesh cable trays and fast-assembly toolless snap-couplers. Pre-galvanized finishes ensure zero zinc-whisker generation, protecting sensitive cloud server racks and telecommunications distribution networks.
Specialized sliding base brackets designed to absorb soil heaving and foundation settlement caused by seasonal permafrost freezing and thawing cycles across remote industrial oilfields.
Complete System Catalog
Full-Spectrum Cable Trays, Fittings & Heavy Support Hardware
Explore our complete inventory of heavy-duty ladder racks, stainless trunking, cold-formed structural brackets, and vibration-proof fastening systems ready for project delivery across Russian industrial zones.
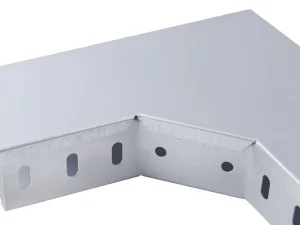
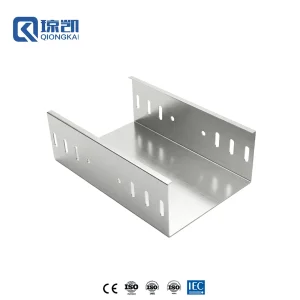
90-Degree Horizontal Bend
Pre-Galvanized Elbow Fitting for Cable Tray
Sturdy formed radius elbows engineered for smooth routing around structural steel columns and equipment skids in commercial and light industrial installations.
How do Qiongkai cable tray accessories withstand Russian winter temperatures of -50°C to -60°C without cold brittleness?
Our engineering team utilizes low-carbon micro-alloyed structural steel grades chemically balanced with low phosphorus (≤ 0.025%) and sulfur (≤ 0.015%), strictly matching the mechanical and chemical parameters of Russian steel standard 09G2S (per GOST 19281-2014). Cold roll-forming and stamping processes are conducted under monitored strain rates to prevent work hardening. Finished accessories undergo Charpy V-notch impact testing at -60°C, consistently achieving impact energy absorption > 34 J/cm². This guarantees that our cantilever brackets, splice plates, and hold-down clamps do not suffer from brittle fracture under dynamic ice or wind loads.
What documentation and quality certifications accompany shipments to the Russian Federation?
Every industrial export consignment is supplied with a comprehensive quality documentation dossier, including:
1. Mill Test Certificate (MTC 3.1): Verifying heat numbers, chemical composition analysis, yield strength (ReH ≥ 235-355 MPa), and tensile elongation.
2. Galvanizing Inspection Report: Documenting magnetic thickness gauge readings across multiple coupon points to guarantee compliance with ISO 1461 (> 65 μm or > 85 μm as specified).
3. EAC / GOST-R Conformity Declaration: Certifying compliance with TR CU 004/2011 (Safety of Low Voltage Equipment) and electrical continuity test reports (≤ 50 mΩ joint resistance).
4. Factory Acceptance Test (FAT) Records: Dimensional inspection protocols and salt spray exposure testing (ASTM B117).
How should engineers calculate thermal expansion and contraction across long Siberian pipe racks?
In regions such as Western Siberia or the Sakha Republic, the ambient temperature difference between summer (+30°C) and winter (-50°C) reaches ΔT = 80°C. The linear thermal expansion of steel is calculated as:
ΔL = α × L × ΔT (where α ≈ 12 × 10&sup6; m/m°C).
For a 100-meter straight cable tray run, ΔL reaches approximately 96 mm. Qiongkai supplies engineered Expansion Splice Plates featuring precision slotted bolt patterns and high-flexibility copper/tinned earth bonding straps. We recommend installing an expansion joint coupler every 30 to 45 meters, accompanied by un-clamped sliding support guides that permit axial movement while preventing lateral derailment.
Which coating is optimal: Pre-Galvanized, Hot-Dip Galvanized (HDG), or Stainless Steel 316L?
Pre-Galvanized (PG, Z275): Optimal for indoor climate-controlled spaces, commercial structures, clean utility vaults, and standard data halls (ISO 12944 Category C1/C2).
Hot-Dip Galvanized (HDG, > 85 μm): The primary workhorse specification for outdoor industrial processing plants, Siberian gas gathering stations, and heavy infrastructure (Category C3/C4). The thick zinc-iron alloy barrier provides sacrificial cathodic protection even if scratched during field erection.
Stainless Steel SS316L (1.4404): Essential for marine coastal LNG export terminals (Yamal, Baltic), offshore platforms, and acid leaching rooms in nickel/copper metallurgy facilities (Category C5-M / CX), offering complete immunity to chloride-induced pitting.
What are the logistics arrangements, lead times, and customs transit points for Russian shipments?
Shanghai Qiongkai leverages multi-modal logistics routes tailored to project urgency and geographical destination:
1. Direct Container Rail Freight: Departs Shanghai/Suzhou directly via the Manzhouli / Zabaikalsk border port into Moscow, Yekaterinburg, and Novosibirsk terminal hubs (transit: 18-24 days).
2. Maritime Sea Freight via Far East: Direct vessel shipment from Shanghai Port to Vladivostok / Vostochny, connecting to the Trans-Siberian Railway network (transit: 10-15 days to port).
3. St. Petersburg Maritime Route: Deep-sea container lines servicing Western Russian industrial zones.
All cargo is crated in fumigated solid timber cases, shrink-wrapped in vapor-barrier polyethene with desiccant packs, and strapped with steel bands to ensure corrosion-free arrival through freezing maritime and rail transit.
Can Qiongkai manufacture customized accessory dimensions and non-standard bracket profiles?
Yes. With our in-house tooling workshop, 60+ heavy stamping machines, and dedicated CNC laser cutting suites, we produce custom-engineered brackets, odd-angle elbows (30°, 45°, 60°), asymmetric reducers, and heavy strut fittings based on customer DXF/DWG drawings or physical benchmark samples. Custom tooling prototyping is completed within 7 to 10 days, followed by full dimensional inspection reports before mass extrusion and roll-forming.
Procure Engineered Cable Tray Accessories for Your Russia Projects
Consult with our structural engineering team today to review load calculations, sub-zero metallurgy compliance, or request an immediate factory-direct commercial quotation.